STD: ASME Sec I & TCVN 7704 // Doc-ref: BKET-ENG-303
Boiler flue-gas heat recovery solution: economizer & air preheater
Recover 60% – 80% of heat lost in flue gas • Cut fuel costs by 10% – 25% • Raise boiler efficiency by 5% – 10%.
Closed-loop operating principle schematic
Convective & radiant heat transfer mechanism for flue-gas heat recovery
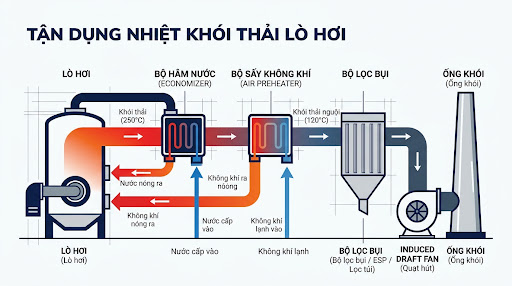
Thermodynamic operating process: Flue gas carrying excess heat from the boiler furnace (initial temperature 220°C – 280°C) first passes through the economizer, transferring heat to the feedwater entering the steam drum (heated from 30°C to 80°C – 105°C). Next, the flue gas flows through the air preheater to heat the combustion air supply (from 30°C to 100°C – 150°C). Finally, the safely cooled flue gas (120°C – 140°C) is drawn by the ID fan through the bag filter/cyclone dust collector before exiting the stack, eliminating the risk of filter bag fires and fan impeller overheating.
01 · Protects the steam drum from thermal shock
Preheating feedwater before it is pumped into the boiler eliminates metal thermal shock at butt welds, reduces uneven thermal expansion, and extends boiler life by decades.
02 · Optimized combustion of wet fuel
Combustion air preheated to 100°C – 150°C makes biomass fuel (wet wood chips, sawdust, rice husk) ignite instantly, lowers the excess air ratio α, eliminates unburned CO and prevents black smoke.
03 · Acid dew point control
BKET engineers precisely calculate the acid dew point (110°C – 118°C) and keep the exit gas at an optimal 125°C – 135°C to maximize heat recovery while eliminating the risk of sulfuric acid (H2SO4) tube corrosion.
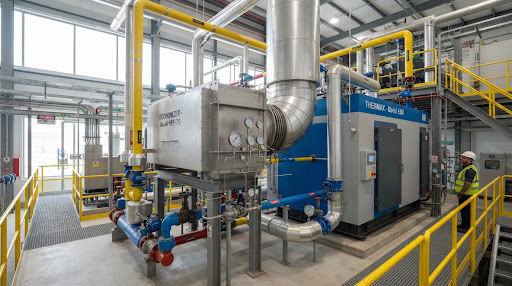
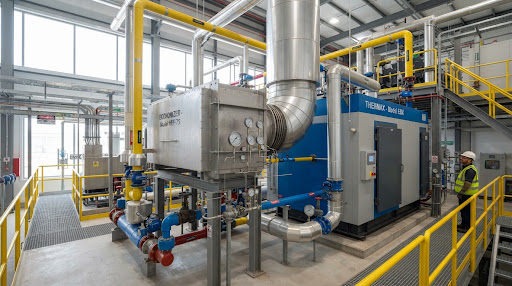 Actual installation: 15 t/h economizer
First heat recovery stage
Boiler economizer
An economizer is a surface heat exchanger that uses heat from the flue gas leaving the boiler’s convection section to preheat feedwater before it enters the steam drum. It cuts fuel consumption by 4% to 8% and eases thermal load fluctuations in the evaporator.
Industrial-grade engineering design
- Load-bearing & insulated casing: Structural steel frame, high-density ceramic/rockwool insulation of 100–120 kg/m³, and outer cladding of color-coated steel sheet or premium 304 stainless steel.
- Heat exchange tube bundle: Specialized high-pressure seamless steel tubes (ASTM A106 Gr.B, 20G) in nominal diameters Ø34, Ø42, Ø49, Ø51 mm, continuously bent with no joints inside the gas stream.
- Spiral/studded finned tubes: Increase heat transfer surface 3 – 5 times compared with plain tubes, reducing equipment size and weight.
- Auxiliary valve system: Equipped with automatic air vents, bottom blowdown valves, water bypass valves, and pressure and temperature gauges at the inlet and outlet.
1. Finned steel tubes
Very high heat transfer coefficient, ultra-compact and lightweight. Suited to oil, gas, fine coal or low-dust biomass boilers.
2. Bare steel tubes
Wide tube pitch minimizes ash and slag buildup. Ideal for fluidized bed boilers firing loose rice husk, peat or sawdust.
3. Cast iron economizer
Fully resistant to SO2/SO3 chemical corrosion when firing high-sulfur FO oil, with an exceptionally long service life.
4. Steaming & non-steaming types
Non-steaming (outlet water 20-30°C below saturation) or steaming type (allows 10-15% of feedwater to evaporate directly).
Design code: TCVN 7704 – 2007
BKET economizer standard specifications
| Boiler capacity range | Heat transfer tube spec | Design pressure | Feedwater ΔT gain | Flue-gas temperature drop | Fuel savings |
|---|---|---|---|---|---|
| 2.0 – 5.0 t/h steam | ASTM A106B Ø34 x 3.5 mm (Finned / Bare) | Up to 16.0 bar | +35°C to +45°C | Reduced by 60°C – 75°C | 3.5% – 5.5% |
| 6.0 – 15.0 t/h steam | ASTM A106B Ø42 x 4.0 mm / Spiral fin | Up to 20.0 bar | +45°C to +55°C | Reduced by 70°C – 85°C | 4.8% – 7.0% |
| 18.0 – 35.0 t/h steam | ASTM A106B Ø51 x 4.5 mm / Multi-path | Up to 25.0 bar | +50°C to +65°C | Reduced by 80°C – 95°C | 5.5% – 8.2% |
Second heat recovery stage
Boiler air preheater (APH)
The air preheater uses the residual heat after the economizer to heat the combustion air (primary & secondary air) up to 100°C – 160°C. This is the key to complete combustion of high-moisture biomass fuel.
Decisive impact on combustion dynamics
Complete burnout of wet fuel
Pre-dries wood chips (35-45% moisture) and fresh rice husk so the fuel ignites instantly on the grate.
Higher furnace temperature
Raises flame temperature by 150°C – 200°C, boosting radiant heat transfer to the water-wall tubes.
Lower q3 & q4 losses
Eliminates chemical and mechanical incomplete-combustion losses; reduces carbon content in fly ash.
No black smoke
Lowers the excess air ratio α and flue-gas volume, reducing ID fan power consumption.
 APH system for a biomass fluidized bed boiler
APH designs manufactured by BKET
Vertical Tubular APH
Vertical tube bundle
Flue gas flows downward inside the tubes, self-cleaning by gravity and highly resistant to clogging.
Horizontal Tubular APH
Horizontal tube bundle
Optimized for boiler houses with limited ceiling height.
Welded Plate Type APH
Welded plate type
Very high heat transfer in a compact volume, with low pressure drop.
Quantitative technical assessment
Performance before and after installing the flue-gas heat recovery system
Field measurement data from a 10 t/h biomass-fired boiler (pellets & wood chips) upgrade project delivered by BKET.
| Operating & measured parameters | Before installation (original boiler) | After installation (BKET economizer + APH) | Measured improvement / benefit |
|---|---|---|---|
| Flue-gas temperature before stack (Tgas) | 255°C – 270°C (high heat loss) | 125°C – 135°C (safe temperature) | ΔT reduced by 130°C (-50%) |
| Feedwater temperature to steam drum (Twater) | 28°C – 32°C (cold tank water) | 95°C – 102°C (via economizer) | Feedwater +68°C |
| Combustion air temperature (Tair) | 30°C (ambient air) | 115°C – 135°C (via APH) | Air temperature +95°C |
| Overall boiler thermal efficiency (η) | 76.5% – 78.0% | 86.2% – 88.5% | Up +8.5% to +10.5% |
| Fuel consumption rate (biomass/ton of steam) | 195 kg pellets / ton of steam | 165 kg pellets / ton of steam | 15.4% fuel savings |
| Fuel cost savings (10 t/h boiler, 20 h/day) | 0 VND (lost directly to atmosphere) | 210,000,000 – 260,000,000 VND / month | Payback in 7.5 months |
| ID fan & bag filter condition | Frequent filter bag fires, fan overheating | 130°C inlet gas: durable, fully stable operation | 100% protection of downstream equipment |
Industry-standard process
5 implementation steps by BKET
An in-depth approach based on actual field measurements, mechanical calculations and guaranteed savings performance before contract signing.
Measurement & survey
A flue gas analyzer (Testo 350) measures flow, gas temperature, and O2, CO and SO2 concentrations, plus a survey of the installation space.
3D & thermodynamic design
Calculation of heat transfer area and aerodynamic pressure drop (ΔP), CFD flow simulation, and detailed fabrication drawings per ASME / TCVN.
Fabrication & hydrotest
Fabricated at the BKET workshop with automatic submerged arc welding, rockwool insulation and hydrostatic testing at 1.5 times design pressure.
Rapid installation (shutdown)
We use the plant’s weekend maintenance shutdown to lift, install and connect the gas, water and air ducts. Zero disruption to production.
Commissioning & guarantee
Boiler test firing, re-measurement of flue-gas and feedwater temperatures, and verification of fuel savings as guaranteed in the contract.
Technical documents
BKET economizer & air preheater (2025)
Sample design drawings, geometric sizing sheets, thermodynamic formulas and test certificates.
Industrial partners who trust BKET technology

BKET technical commitment
Request a free survey & heat recovery assessment
BKET‘s thermal engineering team will visit your plant with dedicated Testo flue gas analyzers to survey, measure and prepare a technical-financial feasibility study (FS), completely free of charge.
- No upfront survey costs.
- 24-month warranty on performance and mechanical durability.
- Minimum fuel savings guaranteed in the EPC contract.
Boiler design & survey information
Please briefly describe your boiler’s current state so our engineers can prepare a preliminary solution.
Bach Khoa Ha Noi Energy Technology JSC
Technical hotline
Technical office
Hanoi & Ho Chi Minh City
Chief engineer hotline: 0247 303 5689 · support@bket.com.vn • Mon – Sat