Industrial energy optimization protocol · ISO 11011 & ISO 50001
Energy optimization solutions for industrial compressed-air systems
Cut air-compressor station power consumption by 15% – 35% • Eliminate 80% – 95% of pressure leak points • Recover 70% – 90% of compressor waste heat as hot water for auxiliary production processes.
Station-wide pressure optimization & real-time interlocked VFD coordination.
Converts oil & compressed-air heat into clean hot water at 60°C – 85°C.
Precise ultrasonic leak detection with Fluke / SDT270 acoustic cameras.
Independent measurement and verification of savings per IPMVP & ISO 11011.
Integrated solution system
4 pillars of compressed-air energy optimization
A closed-loop, integrated approach: optimize supply – control distribution – recover auxiliary energy.
01 · VFD for air compressors
Precisely matches airflow to the shop floor’s actual load, eliminating energy-wasting unload cycles.
02 · Central control (Master Controller)
Intelligent multi-compressor load-balancing algorithm keeps system pressure fluctuation within an ultra-narrow ±0.1 bar band.
Engineering & technology
Detailed analysis of the 4 optimization subsystems
Asynch / PM motorSubsystem 01 · Electronic speed control technology
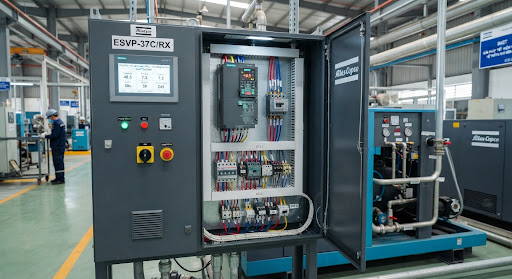
VFD installation for rotary screw air compressors
Most fixed-speed rotary screw compressors operate on a Load / Unload cycle. When unloaded, the motor still draws 40% – 60% of rated power without producing a single cubic meter of air. BKET’s dedicated VFD solution adjusts frequency in real time to precisely match air supply to air demand.
Subsystem 02 · Automation & SCADA dispatch
Compressed-air station central controller (Master Controller)
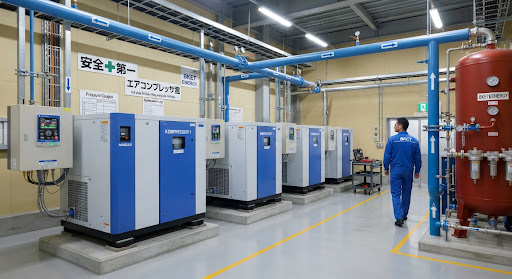
In a station with multiple compressors (2 to 8 units), manual cascade pressure settings often create a wide pressure band (6.8 – 8.2 bar) and several compressors running unloaded at the same time. The BKET Master Compressor Controller uses an intelligent algorithm to select the optimal compressor configuration for the actual load.
Golden engineering rule: Every 1.0 bar (14.5 psi) reduction in system set pressure directly saves approximately 7% of the station’s total energy consumption! The BKET controller safely lowers the pressure band from 8.0 bar to 6.2 bar.
±0.75 bar fluctuation (wasted energy)
Stable within an extremely narrow band
 Multi-compressor
 75°C hot water
Subsystem 03 · Thermal energy recovery
Air-compressor waste heat recovery system
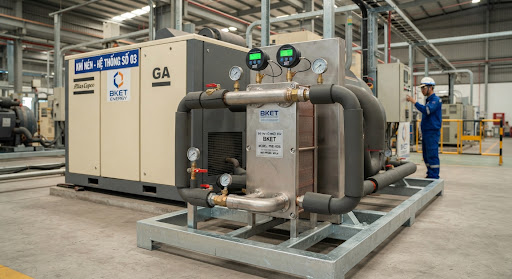
By thermodynamic principles, about 90% – 94% of the electrical energy fed into an air compressor turns into heat that cooling fans discharge to the environment. BKET installs SUS316 stainless steel brazed plate heat exchanger modules to recover heat directly from the compressor’s lubricating oil circuit.
Continuous 60°C – 80°C hot water production
Supplies preheated boiler makeup water (saving biomass/coal/gas fuel) or water for domestic use, pasteurization and food CIP.
Smart automatic thermal bypass valve
Keeps compressor oil temperature within the manufacturer’s standard operating range, fully protecting the compressor motor.
Very fast payback
Payback in just 04 – 08 months when replacing electric heaters or DO/LPG fuel.
Subsystem 04 · Ultrasonic diagnostics
Compressed-air leak scanning & control with acoustic cameras
In industrial plants, compressed-air leaks average 20% to 40% of total compressed-air output! Leaks occur silently at fittings, shutoff valves, drains and hoses. BKET uses Fluke / SDT270 ultrasonic acoustic cameras to visually locate leaks from a distance while the plant is running at high noise levels.
| Hole diameter | Air loss | Wasted power | Annual loss |
|---|---|---|---|
| 1.0 mm | 0.07 m³/min | 0.5 kW | ~ 8,700,000 VND |
| 3.0 mm | 0.65 m³/min | 4.4 kW | ~ 77,000,000 VND |
| 5.0 mm | 1.82 m³/min | 12.2 kW | ~ 213,000,000 VND |
Quantified report for each leak point with acoustic images, GPS coordinates & repair ROI calculation.
 Ultrasound camera
Actual measured data
Before & after optimization performance comparison
Case study: 3 x 75kW industrial compressed-air station (225 kW total) • Operating 24h x 300 days/year.
| Technical metric | Before retrofit | After optimization (BKET) | Results achieved |
|---|---|---|---|
| Station operating mode | 3 compressors running independently, 7.5 – 8.5 bar | Interlocked central coordination, stable at 6.2 bar | 1.3 bar less excess pressure |
| Wasteful unload running ratio | 38% of total run time | Under 5% (thanks to VFD speed control) | 86% lower unload losses |
| Pipe network leak loss ratio | 28% of total compressed-air flow | Under 5% (after fixing 64 leak points) | 23% reduction in artificial demand |
| Heat recovered as hot water for production | 0 liters (heat discharged to atmosphere) | 2,500 liters/hour of 65°C hot water continuously | Hot water for boiler feed |
| Average monthly energy consumption | 135,000 kWh / month | 96,000 kWh / month | Saves 39,000 kWh/month (~28.9%) |
| Direct electricity cost savings | Baseline cost | ~ 78,000,000 VND / month | ROI payback: ~10 months |
International technical standards
5-step ISO 11011 compressed-air station survey & optimization process
Scientific methodology, real measurements with specialized instruments, and transparent data committed before you invest.
7-day 24/7 data metering
Install sensors to continuously measure power (kW), pressure (bar) and flow (m³/min) to build an accurate load profile.
Ultrasonic leak scanning
Survey the entire pipe network, map leaks acoustically, tag each location with an ID and calculate losses.
Simulation & solution design
Engineering calculations combining VFD + Master Controller + heat recovery, plus a pre-feasibility report and payback (ROI) calculation.
Fast installation & retrofit
Rapid mechanical, electrical and integrated control works, planned to avoid interrupting the plant’s production air supply.
Measurement & verification (M&V)
Post-retrofit comparative measurement per the IPMVP protocol, handover of the online SCADA monitoring solution and acceptance.
Field experience
Featured projects at manufacturing plants
Solutions proven in practice at key industrial parks nationwide.
 Mechanical & electronic components
Mechanical & automotive components plant
Installed VFDs & an interlocked Master Controller for a station of 4 x 90kW air compressors. Station energy savings of 24.3%.
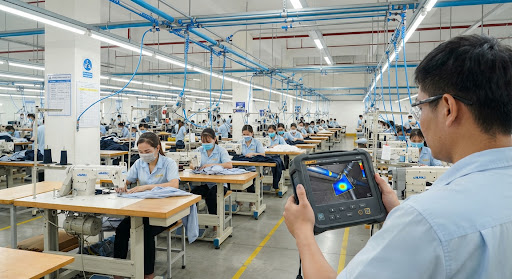 Export textiles & garments
Export textile & garment group
Comprehensive ultrasonic survey and repair of 82 compressed-air leaks across a 2,500m pipe network. Cut power consumption of 3 air stations by 18%.
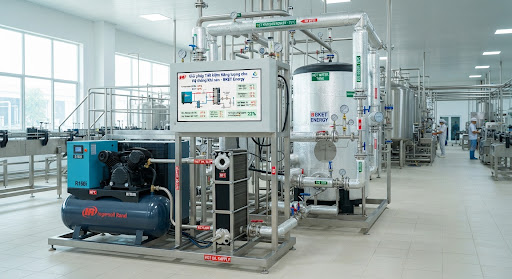 Food processing & F&B
Food & beverage processing plant
Installed a heat recovery unit producing 70°C hot water from 2 x 110kW compressors, feeding the product washing and pasteurization stage directly and replacing a coal-fired boiler.
Industrial clients & partners


Site survey & measurement
Book a free compressed-air station survey & measurement
BKET energy engineers will contact you to confirm details and carry out on-site measurement within 24 business hours. All plant data is kept strictly confidential under an NDA.
Bach Khoa Ha Noi Energy Technology JSC
Technical hotline
Technical office
Hanoi & Ho Chi Minh City